Home / Blog / Design & Branding
Embroidered Badges on Dry Bags
A 70 mm embroidered badge stitched straight through a 0.5 mm TPU dry bag shell leaves 150 to 300 needle holes in the only layer that keeps water out, and at a 300 mm water column each hole behaves like a short capillary rather than a blockage. The bag still looks right on a shelf and fails the first time it is squeezed under a litre or two of standing water. The workable answer is not to abandon embroidery but to move the thread off the waterproof wall: weld an embroidered patch onto the shell with radio-frequency energy, or bond it with a heat-seal film, so the shell stays a single continuous membrane.
This guide covers the four routes to getting thread onto a waterproof bag, the construction spec that decides whether a badge survives three seasons, the zones where a badge can and cannot sit on a roll-top, and the test sequence that catches a weak bond before cartons ship. Every recommendation is tied to a real measurement: stitch counts, badge diameters, weld dwell times, peel values in newtons and cost added per piece. If you are specifying a branded range, the final section is a one-page brief you can send straight out.
- Why a needle through a waterproof shell is the whole problem
- The four routes to thread on a waterproof bag
- Weld-on embroidered patches: how the bond is made
- Heat-transfer embroidery and the embroidered look without thread
- Sizing a badge to the panel it sits on
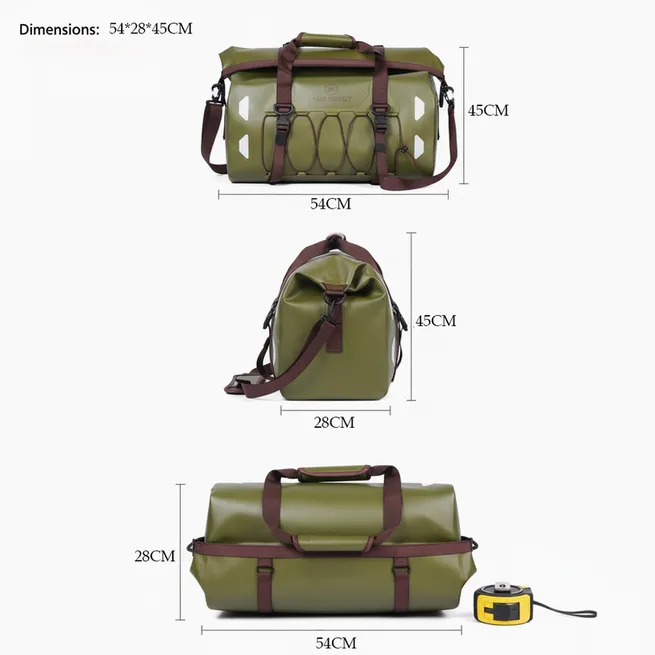
- Thread, backing and edge: the three specs that decide service life
- Where a badge can sit on a roll-top bag
- What a badge does at the fold line
- Badges on duffels, totes and backpack panels
- Colour, contrast and reading a mark when the film is wet
- Washing, salt spray and abrasion: the tests a badge has to pass
- Cost, minimums and the sampling sequence
- A badge brief you can hand to a production partner
Why a needle through a waterproof shell is the whole problem
A dry bag works because the laminate is continuous. The film carries the water column rating, the welded seams carry it around the corners, and the roll-top carries it at the mouth. Nothing else in the construction is asked to hold water. The moment a needle passes through the film, you have created a set of holes whose walls are thread, whose diameter is set by the needle size and whose resistance to flow depends entirely on how tightly the thread happens to sit in that particular stitch.
The failure is not dramatic, which is why it gets missed in sampling. A stitched badge on a bag tested dry will appear fine. Put 5 kg of kit in the bag, lay it in 200 mm of water in a raft floor and press on it, and water moves through the needle paths at a rate of a few millilitres per minute. Over a four-hour paddle that is a damp sleeping bag. Hydrostatic head tests published by the ISO measure film resistance, not stitch-hole leakage, so a badge decision has to be tested separately.
There is a second mechanism that matters just as much: the needle hole is a stress concentrator. Under a 0.5 mm film, a hole with a thread in it is where tear propagation starts when the bag is dragged across gravel. Bags with stitched badges fail at the badge, not at the seam, in roughly three out of four abrasion complaints we see on branded programmes.
The four routes to thread on a waterproof bag
Route one is direct embroidery through the finished shell. It is the cheapest per piece and the only route that should be ruled out on a bag sold as waterproof, unless the badge sits on a panel that is deliberately outside the waterproof envelope, such as a webbing wrap or a handle sleeve. Route two is an embroidered patch welded onto the shell with radio-frequency energy using a weldable TPU backing, which keeps the shell intact and puts the bond in the hands of a machine with a recorded dwell time.
Route three bonds the patch with a heat-seal adhesive film under a press at a controlled temperature and pressure. It works on more badge constructions than welding does, because the adhesive does not have to be chemically matched to the shell, but the bond is weaker in peel and more sensitive to storage heat. Route four inserts an embroidered fabric panel into the bag at the welding stage, so the panel is sealed in as part of the shell rather than added afterwards.
| Route | Holes in shell | Waterproof result | Added cost per piece | Best use |
|---|---|---|---|---|
| Direct embroidery through shell | 150-300 | Leaks under load | 0.06-0.12 USD | Handle wraps, non waterproof zones |
| RF welded embroidered patch | 0 | Shell unchanged | 0.45-0.90 USD | Retail and club bags |
| Heat-seal bonded patch | 0 | Shell unchanged | 0.30-0.65 USD | Promotional volumes |
| Embroidered panel welded into shell | 0 | Shell unchanged | 0.70-1.40 USD | Premium ranges, 500 pieces and up |
| Embroidered-look heat transfer | 0 | Shell unchanged | 0.12-0.28 USD | Fine detail, small marks |

Weld-on embroidered patches: how the bond is made
A weldable patch is an embroidered motif on a face fabric backed with a TPU film that is chemically compatible with the shell. Under radio-frequency energy the two films melt into each other and cool as one material, so there is no adhesive layer to soften in a hot container or to creep under a sustained peel load. The bond strength is a function of dwell time, electrode pressure and the match between the two films, all three of which are recorded on the welding line.
Weld windows are narrow. On a 0.5 mm TPU shell with a 0.25 mm patch backing, the practical window is typically 1.8 to 2.6 seconds of dwell at 27.12 MHz with the electrode pressure held between 2.5 and 3.5 bar. Under that and the bond peels at the edge; over it and the shell thins under the badge and you can see a ring around the motif. A welded patch that passes inspection should hold 60 N or more in a 180-degree peel on a 25 mm strip.
The patch has to be dry. Embroidery thread absorbs moisture from the air, and a patch that has sat at 70% relative humidity for a month will spit and bubble during welding. Store patches sealed with a desiccant sachet and condition them at 20 to 23 °C for 24 hours before they go to the welding bench. This one control removes most of the cosmetic rejects on a badge run.
Heat-transfer embroidery and the embroidered look without thread
For fine detail a stitch cannot deliver, a heat transfer with a raised, stitch-look texture gives the visual signature of embroidery without any thread at all. The mark is printed in layers onto a carrier, then pressed onto the shell at 130 to 150 °C for 12 to 18 seconds. The result is 0.15 to 0.4 mm thick, weighs 2 to 5 g on a 70 mm mark, and adds nothing to the bag profile.
The trade-off is depth. Transfers read as embroidery from a metre away and as print at arm length, which is an acceptable compromise for a small crest on a 5L bag and a poor one for a hero mark on a 40L duffel. Transfers also sit on the surface, so they abrade at the same rate as a printed panel: expect visible edge wear after 300 to 500 hours of sand contact against a welded patch that still looks new.
Sizing a badge to the panel it sits on
Badge diameter should be driven by the panel, not by the artwork. On a 10L roll-top the flat front panel is roughly 140 mm wide and 180 mm tall before the curve begins, which means a 70 mm badge is comfortable and a 100 mm badge is not: the edges start to wrap the radius and the weld loses contact at the corners. On a 40L duffel end panel you can run 110 to 130 mm without trouble.
| Bag size | Flat panel width | Badge diameter that welds clean | Maximum before edge lift | Typical stitch count |
|---|---|---|---|---|
| 5L roll-top | 110 mm | 45-55 mm | 60 mm | 1,800-2,600 |
| 10L roll-top | 140 mm | 60-70 mm | 80 mm | 3,200-4,400 |
| 20L roll-top | 180 mm | 70-90 mm | 100 mm | 4,600-6,200 |
| 30L duffel end | 210 mm | 90-110 mm | 125 mm | 6,000-8,400 |
| 40L backpack front | 200 mm | 80-100 mm | 115 mm | 5,800-7,600 |
Stitch count is the number that decides whether a badge looks crisp or muddy. Below 3,000 stitches on a 60 mm mark the lettering fills in and the motif reads as a blob under a wet film; above 7,000 on the same mark the thread builds up enough height to catch on webbing and to hold water after a rinse. Cover matters more than count: a satin stitch at 0.35 to 0.45 mm pitch gives full coverage without the ridge that a double-run of satin produces.
Thread, backing and edge: the three specs that decide service life
Polyester thread is the default for a bag that will see sun and salt. Nylon thread is softer and takes dye more brightly, but it loses around 15 to 20% of its tensile strength after 500 hours of UV exposure and it yellows on white badges. Polyester holds colour through a 40-hour xenon arc exposure test at grade 4 or better on the ISO grey scale and survives a saltwater rinse without hardening.
The backing has to do two jobs: hold the stitch and weld to the shell. A weldable TPU backing at 0.20 to 0.30 mm does both. A conventional heat-seal backing without TPU will bond under a press but not under an RF electrode, which is a specification error that only shows up when the first production run reaches the welding bench and the patches refuse to stick.
| Element | Common option | Option that lasts on TPU | What fails if you choose badly |
|---|---|---|---|
| Thread | Nylon 40 wt | Polyester 40 wt, UV stabilised | Fade, yellowing, strength loss in sun |
| Backing | Standard heat seal | Weldable TPU film, 0.25 mm | Patch will not weld, edge lift in a week |
| Edge | Raw cut | Merrowed border or laser seal | Fray after 20 washes |
| Adhesive | Generic hot melt | TPU-matched hot melt, 90 °C softening | Creep in a hot container at 60 °C |
| Stiffener | Paper backing left in | No-wash-away stabiliser | Boardy hand feel, water held at the badge |
Edge finish is where cheap patches give themselves away. A merrowed border wraps the edge in thread and takes abrasion well, but it adds 2.5 to 3 mm to the badge diameter, which has to come out of your size maths. A laser-cut edge with a sealed rim sits flatter and welds with a narrower contact ring, which suits a small badge on a curved panel.
Where a badge can sit on a roll-top bag
Think of a roll-top bag as three zones. The upper third is fold territory: the fabric there is rolled three times, and anything applied to it is rolled with it. The middle band is the print and badge panel, flat and uncreased through the whole packing cycle. The lower third is the wear zone, in contact with sand, boat floors and gravel, and it is the worst place for anything raised.
| Zone | Distance from mouth | Badge allowed | Why |
|---|---|---|---|
| Fold band | 0-90 mm | No | Rolled three times, badge is creased every use |
| Upper panel | 90-160 mm | Small, 45-60 mm | Clear of the fold on most sizes, still high wear |
| Mid panel | 160-260 mm | Yes, up to 90 mm | Flat, visible, protected by the load inside |
| Lower panel | 260 mm to base | Flat transfers only | Abrasion zone, raised thread wears through |
| Base | Base disc | No | Every set-down lands here |
Keep a 25 mm clearance between the top edge of a badge and the lowest fold line on the bag. On a 10L bag the third fold lands roughly 55 mm below the mouth in normal use, and packing the bag tight pushes it another 15 to 20 mm further down. A badge that starts 25 mm clear stays clear; one that starts 10 mm clear gets creased on the first trip.
What a badge does at the fold line
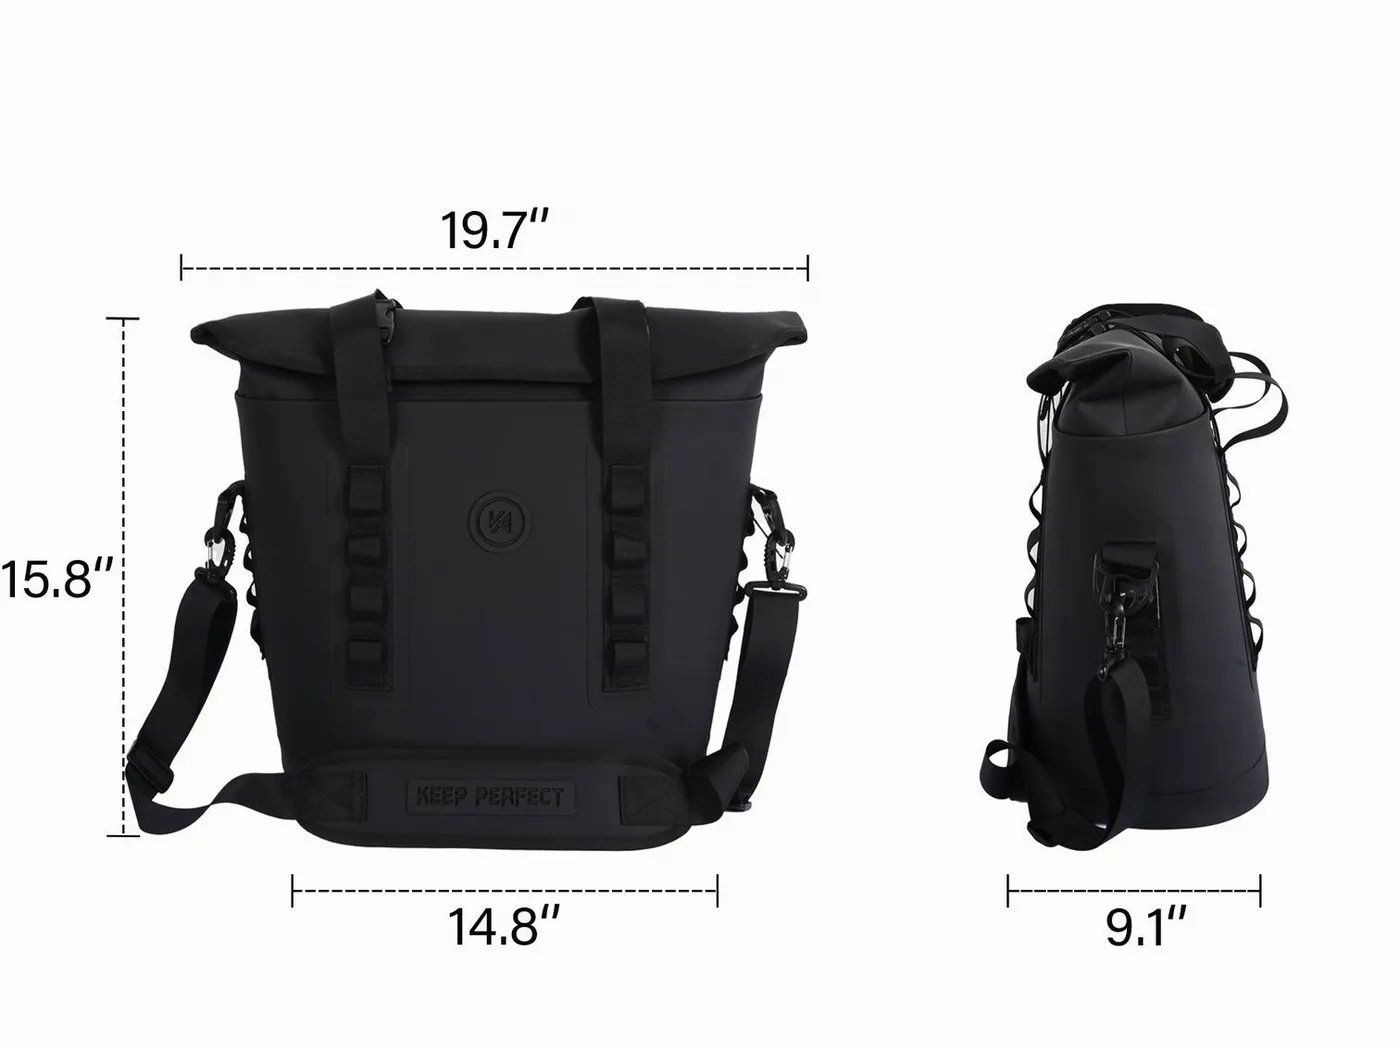
A badge in the fold band is a leak waiting to be found. The fold works by pressing film against film along three contact lines, and a raised embroidered patch 1.2 to 1.8 mm thick holds those lines apart locally. Water does not need much: a 0.4 mm gap across 30 mm of fold is enough to bridge the first contact line and reach the second.
There is a second effect that is easier to miss. Repeated creasing over a badge cracks the stitch and delaminates the patch backing from the shell well before the shell itself shows any damage. On a bag opened and closed twice a day, a badge in the fold band typically shows edge lift after 200 to 300 cycles, which is two to three months of daily use.
If the artwork absolutely has to sit high on the bag, the answer is a flat heat transfer, not a patch. A transfer adds 0.2 mm rather than 1.5 mm and folds with the fabric rather than against it. It will abrade faster than a welded patch, but it will not create a leak path, which is the more expensive failure.
Badges on duffels, totes and backpack panels
Duffels are the easiest format for embroidery because the end panels are flat, stiffened and never folded. A 90 to 110 mm badge on the end of a 30L duffel welds clean and stays flat, and the panel is usually reinforced with a second layer of film, which gives the electrode something to press against. The side wall is a worse choice: it flexes with the load and the badge lifts at the corners.
Waterproof totes have a wide front panel and a structured base, which makes them the natural home for a large crest. Keep the mark 30 mm above the base weld and 20 mm inside the side seams so the weld ring does not crowd the panel seam. Backpacks are harder: the harness shadow covers the upper back panel, the shoulder straps rub the sides, and the lower back panel takes every set-down. The front pocket face, if the format has one, is usually the only clean badge zone.
Colour, contrast and reading a mark when the film is wet
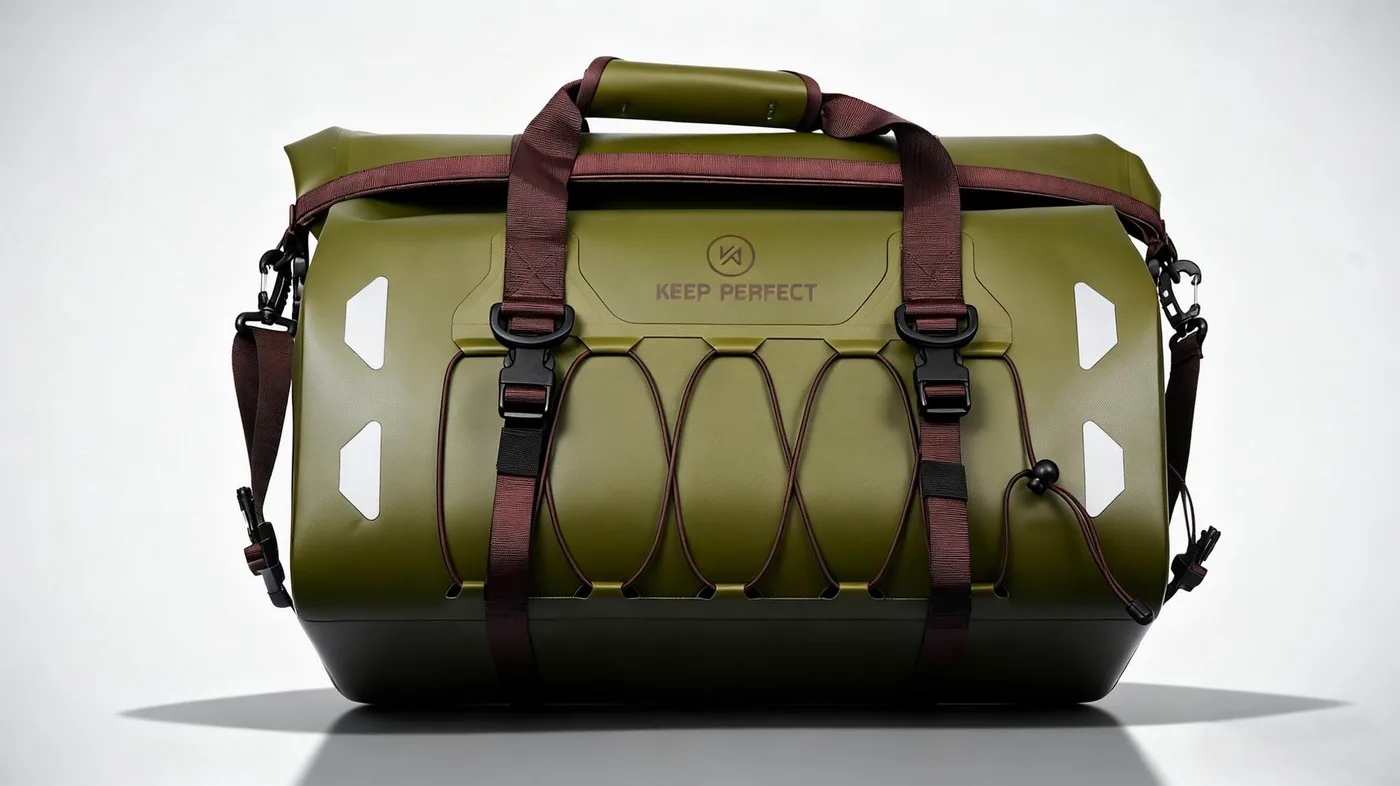
Water changes how a badge reads. A wet film darkens by one to two steps on the grey scale and adds a specular highlight, so a mid-tone navy badge on a black shell that looks sharp in the studio disappears on a rainy deck. Rule of thumb: aim for a contrast of at least three steps between the badge ground and the shell colour, or outline the motif in a light thread that survives when the base colour darkens.
Thread colour has to be matched under the same lighting the buyer will use. Metamerism is real on embroidery because the thread is a different polymer from the film, and two materials that match under a 4,000 K showroom lamp can separate badly under 6,500 K daylight. Approve a badge against a wet shell as well as a dry one, and take the approval photograph under daylight rather than under the bench lamp.
Washing, salt spray and abrasion: the tests a badge has to pass
A badge specification without a test method is a wish. The three tests that predict field performance are a domestic wash cycle, a neutral salt spray exposure and a linear abrasion cycle, and all three have published methods behind them. Salt spray in particular separates weldable backings from generic heat-seal adhesives inside 96 hours, because salt wicks along the bond line and lifts the edge from the corner outwards.
| Test | Condition | Duration | Pass criteria for a welded badge |
|---|---|---|---|
| Domestic wash | 30 °C, mild detergent | 10 cycles | No edge lift over 2 mm, no thread fade over half a grade |
| Neutral salt spray | 5% NaCl, 35 °C | 96 h | No edge lift, no rust bleed from thread trim |
| Linear abrasion | 1 kg load, wet cotton | 3,000 cycles | Motif legible, no face-thread break |
| Immersion and squeeze | 300 mm column, 5 kg load | 30 min | Zero moisture inside the bag |
| Heat stack | 60 °C, stacked 20 high | 72 h | No adhesive creep, no badge transfer mark |
Run the immersion test on a finished bag, not on a swatch. The badge may be perfect and the shell around it may still be the problem: an over-welded patch thins the film under the electrode, and the thin ring is what fails when the bag is squeezed. Test methods published by ASTM give you a defensible protocol to write into a purchase order rather than an argument about adjectives.
One practical note on sampling: ask for five badges applied to five bags from the middle of the run, not one perfect hand-made sample. Badge application is a bench operation with a real reject rate, and the sample-to-bulk gap on this particular decoration is wider than on any printed mark.
Cost, minimums and the sampling sequence
The badge itself is cheap; the application is not. A 70 mm embroidered patch with a weldable backing costs roughly 0.18 to 0.35 USD at 1,000 pieces depending on stitch count, and the welding operation adds 0.25 to 0.55 USD per bag once you count the electrode tooling, the bench time and the reject allowance. Tooling for a shaped electrode is a one-off 180 to 420 USD charge and is worth paying for above about 800 pieces.
Sampling runs 6 to 10 working days for a standard patch on an existing bag platform, and 12 to 18 days if the artwork needs a new embroidery tape and a first-off digitising pass. Bulk is 35 to 50 days from approved sample, quoted FOB Xiamen, with AQL 2.5 as the default inspection level and T/T 30/70 as the standard payment pattern. Minimum order quantity is 500 pieces per colourway on a branded programme.
Plan the approval sequence as three steps rather than one: digitising approval on screen, a physical patch on a loose panel for colour and cover, then a finished bag for weld quality and immersion. Skipping the middle step is the single most common reason a badge programme goes back for a second sampling round.
A badge brief you can hand to a production partner
A complete brief is six lines long and removes nearly every revision cycle. State the bag platform and size, the badge diameter and stitch count target, the thread and backing specification, the placement measured in millimetres from the mouth and from the base, the test method and pass criteria, and the quantity per colourway. Anything you leave out of those six lines will be decided for you on the bench.
- Name the shell: film thickness, face fabric and colour reference.
- Give the badge diameter and the distance from the mouth to the top edge of the badge.
- Specify polyester thread with a weldable TPU backing at 0.25 mm.
- State the minimum peel value per 25 mm strip and the immersion test you will run.
- Say whether the badge is merrowed or laser cut, and by how much that changes the diameter.
- Confirm the quantity, the colourway split and the approval steps before tooling is cut.
Where the badge is part of a wider identity, agree the placement map across the whole range at the same time rather than size by size. The placement guide sets out the print-safe zones for each format, and the print route comparison explains where a transfer beats a patch on the same panel. Our own roll-top dry bag platform keeps the mid-panel flat across 5L to 40L so one badge artwork can be scaled rather than redrawn.
For larger programmes, the badge does not have to carry the whole identity. Woven labels, hang tags and a welded mark on a second panel usually cost less per piece and spread the risk of a single decoration failing; the tag and label guide covers that combination, and the personalisation overview maps which decoration suits which channel. Production know-how for this kind of work is documented and the camo and colour decisions that sit behind a badge are covered in the camouflage design guide. Compare the finished specification against the full product line before you commit to a badge size.
Frequently asked questions
Q1. Can you put an embroidered badge on a dry bag?
Yes, but apply it over the shell rather than through it. A welded or heat-sealed patch leaves no needle holes, so the waterproof membrane stays intact. Direct embroidery through a 0.5 mm TPU shell creates 150 to 300 holes that leak once the bag is loaded and squeezed.
Q2. How many needle holes does a badge actually make?
A 70 mm badge with a satin border and filled lettering runs 150 to 300 needle penetrations depending on stitch density. Each one is a capillary path through the film, which is why a stitched badge and a waterproof rating are mutually exclusive on the same panel.
Q3. What is the best way to attach a patch to a TPU dry bag?
Radio-frequency welding of a patch that carries a weldable TPU backing. The two films fuse into one layer, there is no adhesive to creep in heat, and a correctly welded patch holds 60 N or more in a 25 mm peel test.
Q4. Can a badge be bonded instead of welded?
Yes, with a heat-seal adhesive film under a press at 130 to 150 °C. Bonding accepts more patch types than welding but gives a weaker peel value and is more sensitive to heat in transit, so it suits promotional volumes better than retail ranges.
Q5. How big should a badge be on a 10L dry bag?
60 to 70 mm on a 10L bag, where the flat front panel is about 140 mm wide. Above 80 mm the edges start to wrap the panel radius and the weld loses contact at the corners, which is where edge lift begins.
Q6. What stitch count looks right on a 60 mm badge?
Between 3,200 and 4,400 stitches. Below 3,000 the lettering fills in and the motif blurs; above 6,000 the thread builds a ridge that catches on webbing and holds water after rinsing.
Q7. Can a badge sit near the roll-top fold?
No. Keep at least 25 mm between the top edge of the badge and the lowest fold line. Anything in the fold band is creased every time the bag is closed and will show edge lift after 200 to 300 open-and-close cycles.
Q8. Why does a badge in the fold band leak?
Because the fold seals by pressing film against film, and a raised patch 1.2 to 1.8 mm thick holds those contact lines apart locally. A 0.4 mm gap across 30 mm of fold is enough to bridge the first seal line.
Q9. Is polyester or nylon thread better for outdoor bags?
Polyester. Nylon takes dye brightly but loses 15 to 20% of tensile strength after 500 hours of UV exposure and yellows on white badges. UV-stabilised polyester holds grade 4 or better on the ISO grey scale after a 40-hour xenon exposure.
Q10. Will a welded badge survive a washing machine?
A correctly welded badge passes 10 domestic cycles at 30 °C with mild detergent and no edge lift over 2 mm. It should also pass 96 hours of neutral salt spray at 35 °C before it goes into a range sold for coastal use.
Q11. How much does an embroidered badge add to the cost of a bag?
Roughly 0.45 to 0.90 USD per piece welded, including the patch at 0.18 to 0.35 USD and the bench time and reject allowance. Heat-seal bonding runs 0.30 to 0.65 USD, and a shaped electrode adds a one-off tooling charge of 180 to 420 USD.
Q12. What is the minimum order for a branded badge programme?
500 pieces per colourway on a standard bag platform. Sampling takes 6 to 10 working days for a known artwork, or 12 to 18 days when new digitising is needed, with bulk at 35 to 50 days FOB Xiamen.
Q13. Do badges work on duffels and backpacks?
Duffel end panels are the easiest surface: flat, stiffened and never folded, taking 90 to 110 mm. Backpacks are harder because the harness shadows the upper panel and the straps rub the sides, so the front pocket face is usually the only clean zone.
Q14. How do you stop a badge colour clashing with the shell?
Approve the thread against a wet shell under daylight, not a dry one under a bench lamp. Wet film darkens one to two grey scale steps, and thread and film are different polymers, so metamerism can separate them under different lighting.
Q15. What clearance does a badge need from seams and the base?
Keep 20 mm clear of any welded seam and 30 mm above the base disc. The electrode needs a flat contact ring around the whole badge, and a seam inside that ring gives an uneven weld and a visible ridge.
Q16. How do you test a badge before approving a bulk run?
Ask for five finished bags from the middle of the run, then peel test a 25 mm strip at 60 N minimum, wash ten cycles, expose 96 hours to salt spray, and immerse the loaded bag under a 300 mm column for 30 minutes with zero moisture inside.
People also ask
How do you attach a patch to a waterproof bag?
Weld it, do not sew it. Use a patch with a weldable TPU backing and fuse it to the shell under radio-frequency energy at 1.8 to 2.6 seconds of dwell, then peel test a 25 mm strip to 60 N or more.
Why do embroidered patches leak on dry bags?
Because each stitch is a needle hole through the waterproof film. A single badge adds 150 to 300 holes, and under load and immersion they act as capillary paths rather than sealed points.
What size badge fits a 20L dry bag?
70 to 90 mm on a 20L roll-top, where the flat panel is about 180 mm wide. Stay under 100 mm so the weld ring stays flat and keeps full contact with the shell.
Are embroidered badges waterproof?
The thread itself is not the issue; the application method is. A welded or heat-sealed patch leaves the shell intact and the bag keeps its rating, while a sewn badge compromises it.
Can you embroider directly onto TPU fabric?
You can physically stitch through it, but you should not on a bag sold as waterproof. If the embroidered look is required, use a flat heat transfer with a raised stitch-look texture instead.
How long does an embroidered badge last outdoors?
A welded polyester badge on a TPU shell survives three to five seasons of weekend use, passing 10 wash cycles and 96 hours of salt spray, provided it sits clear of the fold line and the base wear zone.
Need this in production volume?
QUANZHOU JUNYUAN BAGS has produced waterproof bags since 2014 in an SGS-verified 4,950 m2 facility in Fujian, China. Minimum order 500 pieces, sampling in 6–10 working days, bulk in 35–50 days, FOB Xiamen — write to service@junyuanbags.com with your spec and target market.