Home / Blog / Buying & Comparisons
From Sample to Bulk: Dry Bag Timeline
A first dry bag order takes about 60 to 75 days from a signed brief to a loaded container: 6 to 10 working days for sampling, 10 to 20 days for revision and approval, 35 to 50 days for bulk production, and 5 to 8 days for inspection, packing and documentation. Programmes that reorder an existing specification compress that to roughly 45 days because sampling and tooling drop out entirely. The four variables that break the schedule are fabric lead time, colour matching, print setup and inspection slot availability, in that order of frequency.
This guide walks the eight gates in sequence, compares the three sampling routes against cost and risk, and shows where the 35 to 50 bulk days actually go, process by process. It also sets out what a first sample can and cannot prove, how to place testing inside the sample window rather than after it, and which decisions have to be locked before day one rather than discovered in week three. Every number here is a working figure from real programmes, not a best case.
- The eight gates between a brief and a container
- Days 0 to 3: the brief and the fields that block everything
- Days 4 to 10: sampling and what a first sample proves
- Three sampling routes compared
- Days 11 to 20: revision and the courier clock
- Testing inside the sample window
- Days 21 to 28: approval, the golden sample and the deposit
- Bulk: where 35 to 50 days actually goes
- Material lead time: the variable most plans miss
- Branding steps inside the same window
- Inspection: what AQL 2.5 means for your calendar
- Packing, documents and the FOB handover
- What actually delays a first order
The eight gates between a brief and a container
A programme moves through eight gates: brief, specification lock, sampling, revision, testing, approval with golden sample, bulk production, and inspection with release. Each gate has a deliverable and each one can be passed or failed in a day or can sit open for three weeks. The discipline that keeps a schedule intact is refusing to start the next gate until the previous one has a signed deliverable.
The reason to name them as gates rather than phases is that gates have owners. A brief that is still changing on day nine is not a slow sampling process; it is an open gate one, and no amount of pressure on the production floor recovers those days. Most slipped schedules are traced back to a gate that was treated as informally closed.
Timelines also differ by whether the specification is new. A stock specification in a stock colour with a print logo follows the fast path; a new size, a matched colourway or a welded badge adds tooling and material lead time that no amount of urgency removes. Choosing between those paths is the first decision, and it is worth doing on day one rather than day eleven.
Days 0 to 3: the brief and the fields that block everything
A workable brief is one page: size family, film thickness and face fabric, seam construction, closure geometry, hardware grade, colour references, branding method and artwork, target quantity, target landed cost and the test standards the market requires. Twelve fields, all of which are covered in the spec sheet guide. Missing any one of them does not stop sampling; it stops approval, which is worse because the delay lands later.
Three fields block hardest when they are vague. Fabric specification blocks material ordering, because mills quote lead time against a named construction and a grams per square metre figure. Colour reference blocks dyeing, because a matched shade needs a lab dip cycle. Test standard blocks the schedule outright, because arranging third-party testing after a sample is built adds 7 to 12 days that could have run in parallel.
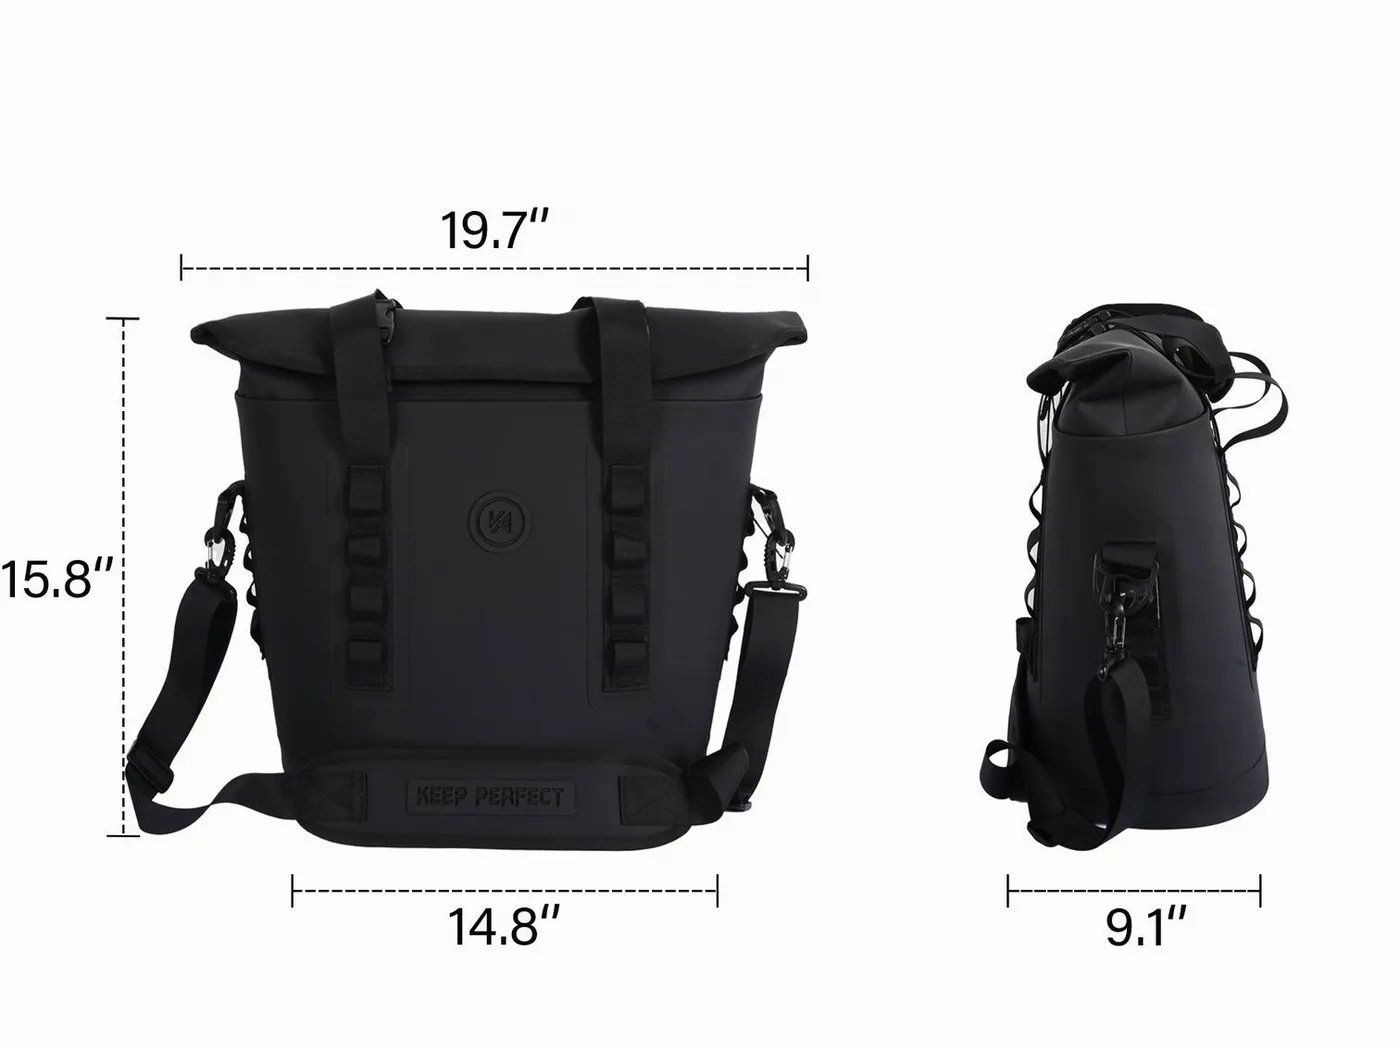
Quantities matter earlier than buyers expect. A 500-piece minimum is not just a commercial threshold; it determines whether a mill will run a matched colour at all, because most fabric lots have a minimum dye quantity of 300 to 600 metres. Deciding quantity in the brief rather than after sampling is what keeps the colour route open.
Days 4 to 10: sampling and what a first sample proves
Sampling runs 6 to 10 working days for a roll-top bag built on existing tooling, measured from specification lock rather than from first contact. That window covers pattern cutting, welding setup, hardware sourcing, assembly and an internal water test. It is a genuine production step, not a mock-up, which is why a first sample is worth far more than a rendering or a modified stock item.
| Sample stage | Working days | What it proves | What it cannot prove |
|---|---|---|---|
| Specification lock | 1-2 | Dimensions, materials, tolerances | Market acceptance |
| Pattern and weld setup | 2-3 | Seam geometry, weld width | Long-term seam fatigue |
| Assembly and trim | 2-3 | Closure feel, hardware fit | Hardware corrosion life |
| Internal water test | 1 | Closure seals under immersion | Third-party certification |
| Photography and dispatch | 1 | Appearance, colour in daylight | Colour match across a re-order |
The honest limitation is fatigue and corrosion. A sample proves the bag is built as specified and that it seals today; it does not prove the weld survives 500 fold cycles or that a buckle survives a season of salt. Those are either accelerated laboratory tests, which take days and cost money, or they are field trials, which take months. Build the decision around what the sample can actually show.
Three sampling routes compared
There are three ways to reach an approved sample and they differ by a factor of four in both time and cost. The route choice is the single biggest lever on the whole timeline, and it is usually made implicitly by whoever writes the brief. Making it explicit is worth an hour of discussion in week one.
| Route | Tooling | Sample lead | Unit cost effect | Risk |
|---|---|---|---|---|
| Stock specification, stock colour | None | 5-7 days | Baseline | Lowest, but limited differentiation |
| Stock specification, matched colour | Dye lot | 10-14 days | +4 to 8% | Lab dip can miss by one shade |
| New size or geometry | Cutting dies, weld jigs | 18-25 days | +12 to 20% | Weld parameters need re-tuning |
| New closure or hardware | Injection tooling | 30-45 days | +25 to 40% | Highest; only for large programmes |
The middle route is where most successful first programmes sit: a proven geometry in a matched colour with printed branding. It buys genuine differentiation at a 10 to 14 day sample lead and avoids the weld re-tuning that makes a new geometry unpredictable. New tooling only pays back above roughly 20,000 pieces across the life of the programme.
Cost effect deserves a caveat. The percentages above are unit-cost effects at a 500-piece quantity; at 5,000 pieces the tooling route amortises far better and the gap narrows to under 10%. Planning a range rather than a single bag changes the arithmetic again, because tooling is shared across sizes. See building a product line for that calculation.
Days 11 to 20: revision and the courier clock
Assume one revision round and budget for two. A first sample rarely closes: the fold feels stiff, the strap sits 20 mm off, the colour reads warmer under retail lighting. Each round costs 6 to 10 working days of build time plus 3 to 5 days of courier time each way, which is why a two-round plan lands at about day 20 rather than day 12.
Compress this by sending a consolidated change list rather than sequential notes. Three emails with one change each produce three sample rounds; one email with six marked-up changes produces one. Photograph the sample against a ruler and mark changes directly on the image, because written descriptions of dimension changes are the most common source of a second unnecessary round.
Courier choice is a real lever. Express air at 3 days costs roughly triple a 5 to 7 day economy service but buys back four days of calendar on each leg. On a 60-day programme that is 7% of the schedule for a small fraction of unit cost, which is usually a good trade when a retail launch date is fixed.
Testing inside the sample window
Testing should run in parallel with revision, not after approval. Send two or three units to the laboratory with the first revision sample and the report lands while the second round is being built. Arranged after approval, third-party testing adds 7 to 12 days of dead time to every programme, and it is the most common avoidable delay in the calendar.
| Test | Duration | Standard | Typical pass criterion |
|---|---|---|---|
| Immersion, IPX7 | 2-3 days | IEC 60529 | No ingress after 30 min at 1 m |
| Water jet, IPX6 | 1-2 days | IEC 60529 | No ingress after 3 min |
| Hydrostatic head | 1 day | ISO 811 | No penetration at 5,000 mm |
| Martindale abrasion | 3-5 days | ASTM D4966 | No film loss at 20,000 cycles |
| Salt spray on hardware | 4 days | ISO 9227 | No red rust at 48 hours |
The IEC publishes the ingress protection grading in IEC 60529 and the ISO publishes the water resistance and corrosion methods most buyers recognise. Naming the standards in the brief means the laboratory can quote and schedule immediately, shaving two or three days off the window.

Testing costs are usually a few hundred currency units per standard and they are the cheapest insurance in the programme. A failed immersion test on a bulk shipment costs more than the entire testing budget, and a dated report from a named laboratory also settles retail buyer questions before they are asked. More on the commercial value is in the tested rating guide.
Days 21 to 28: approval, the golden sample and the deposit
Approval is a physical act, not an email. Two or three identical samples are signed, one is retained by the buyer, one by the production team, and they carry the version number of the approved specification. Any later dispute about colour, weight or weld width is settled by comparing a bulk unit against that physical reference, which is why the golden sample has to be sealed and dated rather than left on a desk.
Commercial terms close in the same week. A 30/70 structure, 30% deposit with the order and 70% against the bill of lading, is standard for a first programme, with FOB Xiamen the usual delivery term. Bulk scheduling starts on receipt of the deposit and of the signed sample, whichever is later, so a delay on either side shifts the production slot rather than just the paperwork.
Bulk: where 35 to 50 days actually goes
Bulk production for a roll-top bag takes 35 to 50 days from slot confirmation. The range is wide because material arrival and line scheduling sit outside the assembly time itself. A programme with stock fabric in a stock colour lands at the short end; a programme waiting on a dyed lot or an injection-moulded buckle lands at the long end, usually without anybody having made a decision to add the time.
| Process | Days | Note |
|---|---|---|
| Material receipt and inspection | 3-6 | Includes gsm check and shade check |
| Cutting | 2-4 | Die cutting of panels and webbing |
| Printing or branding | 3-6 | Adds time only if artwork is on the bag |
| RF welding and assembly | 10-16 | The core of the schedule, 7 lines |
| Hardware and trim fitting | 3-5 | Buckles, D-rings, straps |
| Water test on the line | 2-3 | Sampled per batch, not per piece |
| Packing and carton marking | 2-4 | Barcode, carton labels, palletising |
| Final inspection and release | 3-5 | AQL 2.5, booked in advance |
The two lines that surprise buyers are printing and final inspection. Printing is often assumed to be free of schedule cost because it takes minutes per bag, but setup, curing and re-handling add 3 to 6 days across a run. Final inspection is booked in a queue, and a slot booked at approval rather than at packing saves 3 to 5 days.
Material lead time: the variable most plans miss
Fabric is the longest lead item in most programmes and the one least visible in a production plan. A stocked TPU laminate in a common colour ships in days; a matched shade needs a dye lot with a mill minimum, and a technical film with UV stabilisers or a specific cold-crack rating can take three weeks before it reaches the cutting table.
| Material | Typical gsm | Lead time | Minimum per colour |
|---|---|---|---|
| Stock TPU laminate, black | 430 gsm | 3-5 days | None |
| Stock TPU laminate, colour | 430 gsm | 10-16 days | 300-600 m |
| Matched bespoke shade | 430-620 gsm | 18-28 days | 600-1,200 m |
| Recycled rPET face laminate | 410 gsm | 14-24 days | 600 m |
| Injection-moulded buckle | n/a | 20-30 days | 5,000 pieces |
Ordering material against the approved sample rather than against the purchase order is the shortcut that causes the most damage. It saves a week on paper and risks a shade that was never approved, which surfaces at final inspection when the entire run is already built. Material booked at approval, with the golden sample shade reference attached, is the safe sequence.
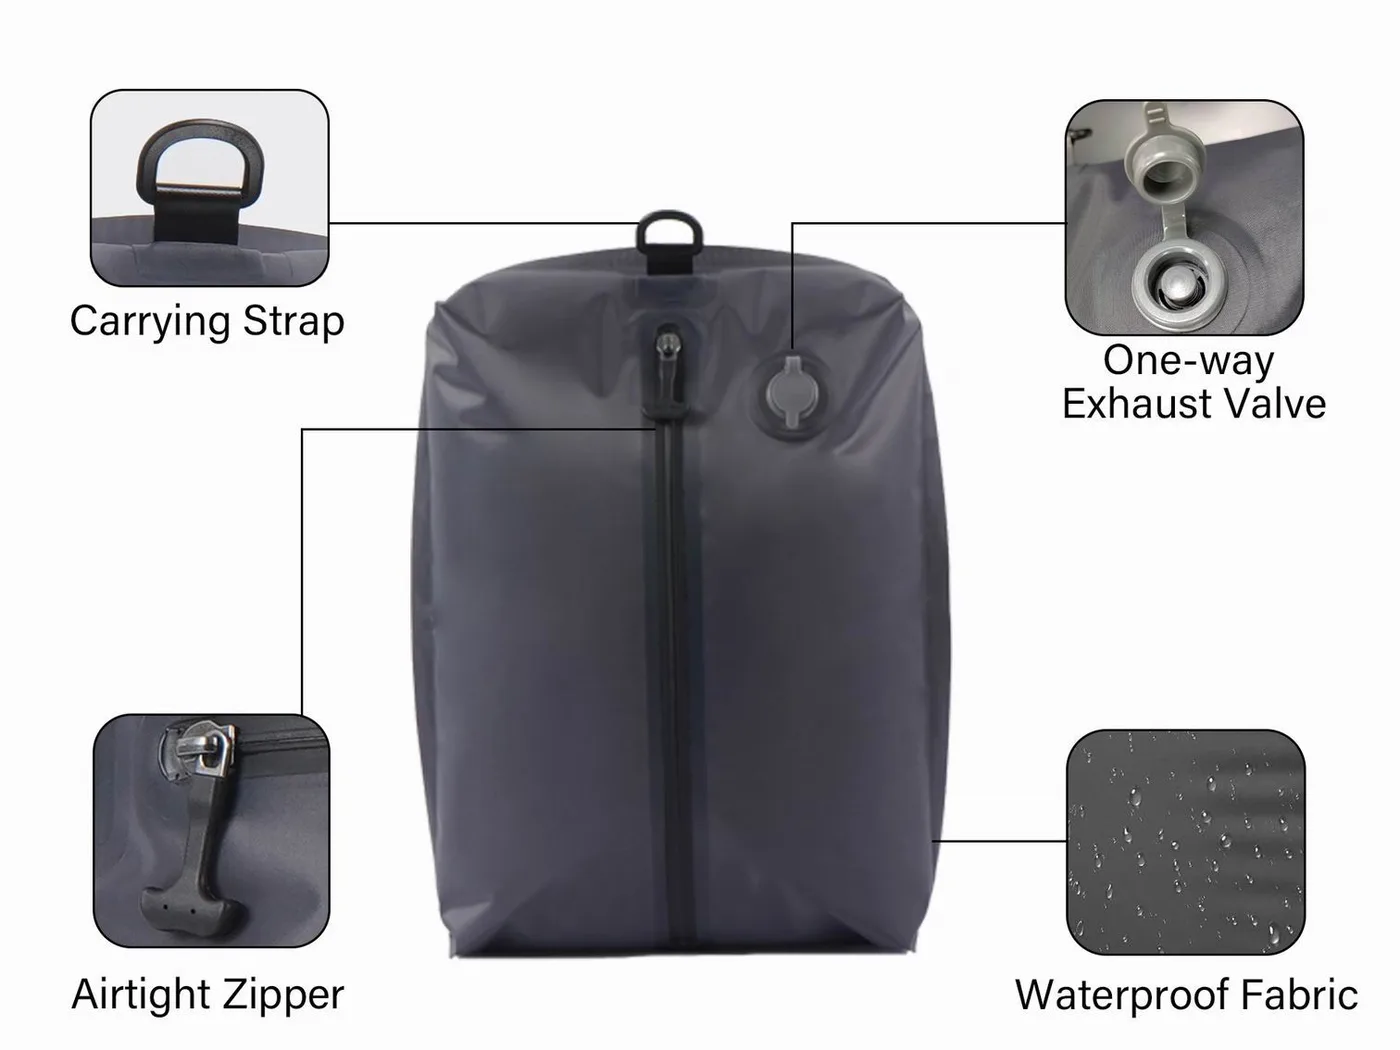
Branding steps inside the same window
Branding runs inside the bulk window if artwork is locked at approval, and it becomes the critical path if it is not. Screen printing needs screens made and colour-separated artwork, digital transfer needs a colour-managed file and a substrate test, and a welded badge needs a tool. Any of these started after approval adds 5 to 10 days to the run.
- Screen print: artwork locked at approval, screens made in 2 days, 1.5 mm minimum stroke, adds 3 working days.
- Digital transfer: colour-managed file, substrate test on the actual laminate, adds 1 working day.
- Woven label: woven to order, 8 mm minimum text height, adds 3 to 5 working days.
- Welded badge: tooling required, 20 mm minimum diameter, adds 5 to 10 working days.
- Reflective transfer: positioned clear of fold lines, adds 3 working days.
One constraint catches people out: artwork cannot cross a fold line. A logo placed where the bag rolls cracks within a season, and a placement discovered to be wrong after printing has started costs a full re-run. Check placement against the rolled sample, not the flat drawing, before screens or tools are made. The detail is covered in the logo placement guide.
Inspection: what AQL 2.5 means for your calendar
AQL 2.5 defines how many minor defects are tolerated in a sampled inspection; it does not mean 2.5% of the shipment may be defective. For a 500-piece order the standard general inspection level II sample is 50 pieces, with 3 minor defects accepted and 5 rejecting the lot. Understanding that number prevents the two common errors: assuming inspection catches everything, and panicking at a single minor finding.
Inspection is a booked slot, not an on-demand service. Booking at approval rather than at packing keeps the release inside the 35 to 50 day window; booking late typically adds 3 to 5 days and, more expensively, can delay the vessel. For waterproof products the inspection should always include a water test on sampled units, because a visual check cannot find a weld that seals under the eye and leaks under pressure.
The full sampling logic and what to do when a lot is rejected is set out in the AQL inspection guide, and the production-side checks that run before inspection are described in quality control for waterproof bags. Both are worth reading before the schedule is agreed, because each adds steps that occupy calendar time.
Packing, documents and the FOB handover
Release is not the end. Packing list, commercial invoice, certificate of origin, test reports and any compliance declarations have to match the shipment exactly, and a mismatch between the packing list and the physical carton count is the most common cause of clearance delay at the border. Budget 2 to 3 days for document preparation and a further day for the freight forwarder to book.
Carton data finalised at approval keeps this stage quiet. Pieces per carton, carton dimensions, gross and net weight, and container loading are needed by the forwarder before the vessel is booked, and a late change from a heavier fabric selection ripples into freight cost. Our programmes standardise on 40 pieces per carton at a 12.4 kg gross weight, which keeps manual handling under the 15 kg limit most warehouses impose.
What actually delays a first order
- A brief that is still changing after sampling has started.
- Colour references without a substrate note, producing a lab dip that misses.
- Third-party testing arranged after approval instead of during revision.
- Artwork delivered late, or placed across a fold line and needing rework.
- Material ordered against a purchase order rather than the approved shade.
- Inspection booked at packing rather than at approval.
- Freight booked before carton data is final, causing a re-quote.
- Payment timing, because production slots are held for a limited period.
Every item on that list is a decision, not an event, and each one can be pre-empted in week one. The programmes that run to 60 days are not the ones with the most experienced buyers; they are the ones where the twelve specification fields were locked before the first sample was cut. If you are planning a smaller first run, small-batch order planning sets out how the same gates compress at lower volume, and quality signals in a sample shows what to check before you sign the golden sample. Our team has produced waterproof bags since 2014 in an SGS-verified 4,950 m2 facility with 7 production lines, a 500-piece minimum and bulk in 35 to 50 days.
Two closing practicalities. First, hold one extra week in the plan for the unexpected, because a programme with no buffer is a programme that will miss a launch date by three days rather than hit it. Second, treat the first order as the expensive one: sampling, testing and tooling are front-loaded, and the second order on an approved specification typically runs 40 to 45 days with no sampling gate at all. Specifications for every size sit in the product line, and commercial questions can go straight to the contact page or the programme FAQ.
Frequently asked questions
Q1. How long does a dry bag order take from sample to bulk?
About 60 to 75 days for a first order: 6 to 10 working days sampling, 10 to 20 days revision and approval, 35 to 50 days bulk, and 5 to 8 days inspection and packing. A reorder on an approved specification runs 40 to 45 days.
Q2. What is the fastest route to a first sample?
A stock specification in a stock colour with printed branding: 5 to 7 days for the sample, no tooling, and the lowest risk. A matched colour adds 4 to 8% to unit cost and 10 to 14 days to the sample window.
Q3. Why does bulk production take 35 to 50 days?
Because only 10 to 16 of those days are welding and assembly. Material receipt, cutting, printing, hardware fitting, water testing, packing and inspection occupy the rest, and material lead time is the widest variable.
Q4. When should third-party testing be booked?
During the revision window, using the first revision sample. Booking after approval adds 7 to 12 days of dead time, because immersion testing alone takes 2 to 3 days and salt spray takes 4.
Q5. What is a golden sample and why does it matter?
A signed, dated physical sample retained by both sides, carrying the version number of the approved specification. It settles any later dispute about colour, weight or weld width by comparison rather than by email.
Q6. How many revision rounds should I plan for?
Budget for two. Each round costs 6 to 10 working days of build plus 3 to 5 days of courier each way, so a two-round plan lands around day 20. Send a consolidated change list to avoid a third.
Q7. What does AQL 2.5 actually mean?
It is a sampling threshold, not a defect allowance. On a 500-piece order at general inspection level II, the sample is 50 pieces, with 3 minor defects accepted and 5 rejecting the lot for rework or re-inspection.
Q8. Does printing add time to the bulk run?
Yes, 3 to 6 days. Screen setup, curing and re-handling add up across a run even though each bag takes seconds to print. Welded badges add 5 to 10 days because tooling has to be made.
Q9. Which material has the longest lead time?
A matched shade, at 18 to 28 days with a 600 to 1,200 metre minimum per colour. Injection-moulded hardware is comparable at 20 to 30 days, but it is needed in smaller volumes.
Q10. What payment and delivery terms are standard?
A 30% deposit with the order and 70% against the bill of lading, on FOB terms, is the usual structure for a first programme. Production scheduling starts on the later of the deposit and the signed sample.
Q11. How do I compress the timeline without cutting tests?
Lock all twelve specification fields before sampling, use a stock geometry, run testing in parallel with revision, book inspection at approval, and use express courier for samples. None of those steps remove a test.
Q12. Can I add a second size late in the process?
Usually yes, because a size family shares material and tooling, so a second size costs days rather than weeks. It is far cheaper than adding a second colourway, which needs its own dye lot.
Q13. What is the minimum order quantity?
500 pieces for most programmes. The threshold is not only commercial: fabric mills typically need 300 to 600 metres per colour, which is the quantity that makes a matched shade viable at all.
Q14. How long does inspection take?
Two to three days on site, but booking is the constraint. A slot reserved at approval keeps release inside the bulk window; a slot requested at packing typically adds 3 to 5 days and can miss the vessel.
Q15. What documents are needed before shipment?
Packing list, commercial invoice, certificate of origin, test reports and any compliance declarations, all matching the shipment exactly. Budget 2 to 3 days, plus a day for the forwarder to book.
Q16. Why do first orders slip more than reorders?
Because sampling, testing and tooling are front-loaded and each has a queue. Once a specification is approved with a golden sample, the second order drops the entire sampling gate and the material is a known quantity.
People also ask
How long does it take to produce dry bags?
A first order takes 60 to 75 days end to end, of which 35 to 50 are bulk production. A reorder on an approved specification takes about 40 to 45 days because sampling and tooling drop out.
What is the sampling process for a waterproof bag?
Specification lock, pattern and weld setup, assembly and trim, internal water test, then photography and dispatch. Six to ten working days for an existing geometry, eighteen to twenty-five for a new one.
Why is bulk production slower than expected?
Because welding and assembly are only 10 to 16 of the 35 to 50 days. Material receipt, printing, hardware fitting, water testing, packing and inspection fill the rest.
Can testing happen during sampling?
Yes, and it should. Send two or three units from the first revision sample to the laboratory so the report lands while the second round is being built, saving 7 to 12 days.
How do you speed up a bag production timeline?
Lock the specification early, use a stock geometry in a stock colour, run testing in parallel with revision, book inspection at approval, and use express courier for sample rounds.
What is the minimum order for a first dry bag run?
500 pieces in most programmes, driven as much by the fabric mill minimum of 300 to 600 metres per colour as by production economics.
Need this in production volume?
QUANZHOU JUNYUAN BAGS has produced waterproof bags since 2014 in an SGS-verified 4,950 m2 facility in Fujian, China. Minimum order 500 pieces, sampling in 6–10 working days, bulk in 35–50 days, FOB Xiamen — write to service@junyuanbags.com with your spec and target market.